Quality assurance


Quality by design, not by chance.
At Advance Paper Box Ltd., quality is built into every stage of our process - from structural design through to final inspection -ensuring consistent, reliable, food-safe cartons in every run.

Our process includes:

Incoming materials quality verification
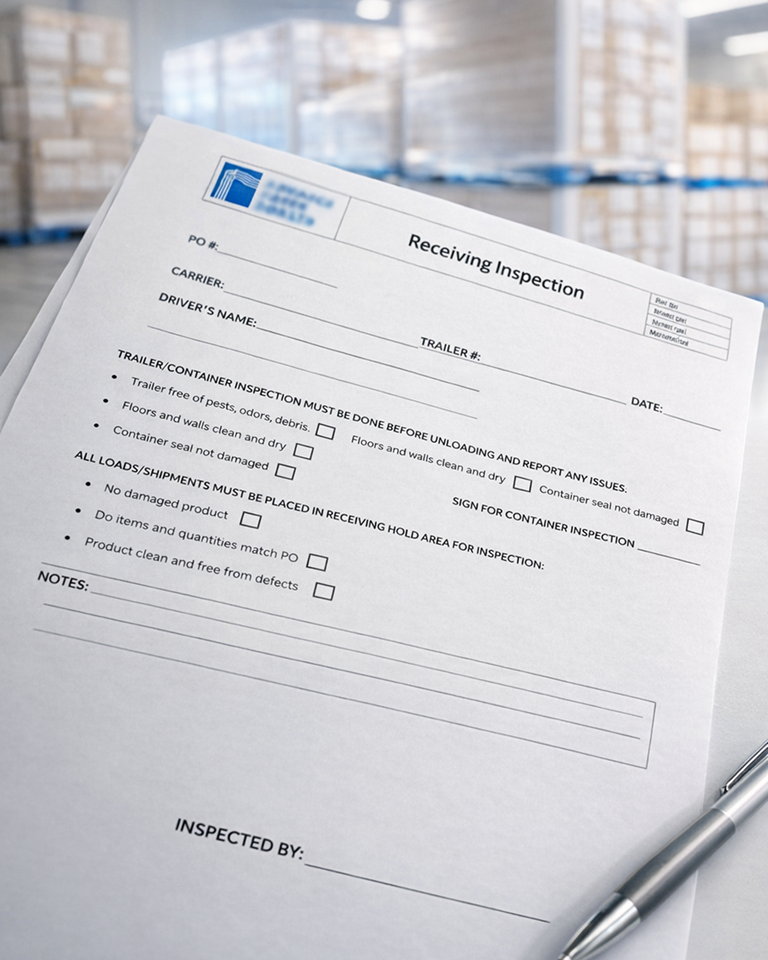
The first step in our quality assurance process includes inspection of all raw materials upon arrival at the plant. This includes a visual inspection of paperboards, inks, adhesives and coatings. Paper rolls are inspected for any visible damage such as crushing or warping. All inks, adhesives, and coatings are visually inspected to ensure they meet required quality standards. Materials are checked for contamination or separation, and any inconsistence in appearance or consistency. The inspection results are documented on the appropriate paperwork. Any materials that do not meet specifications are recorded and placed on hold until corrective action is taken.

In-process quality assurance
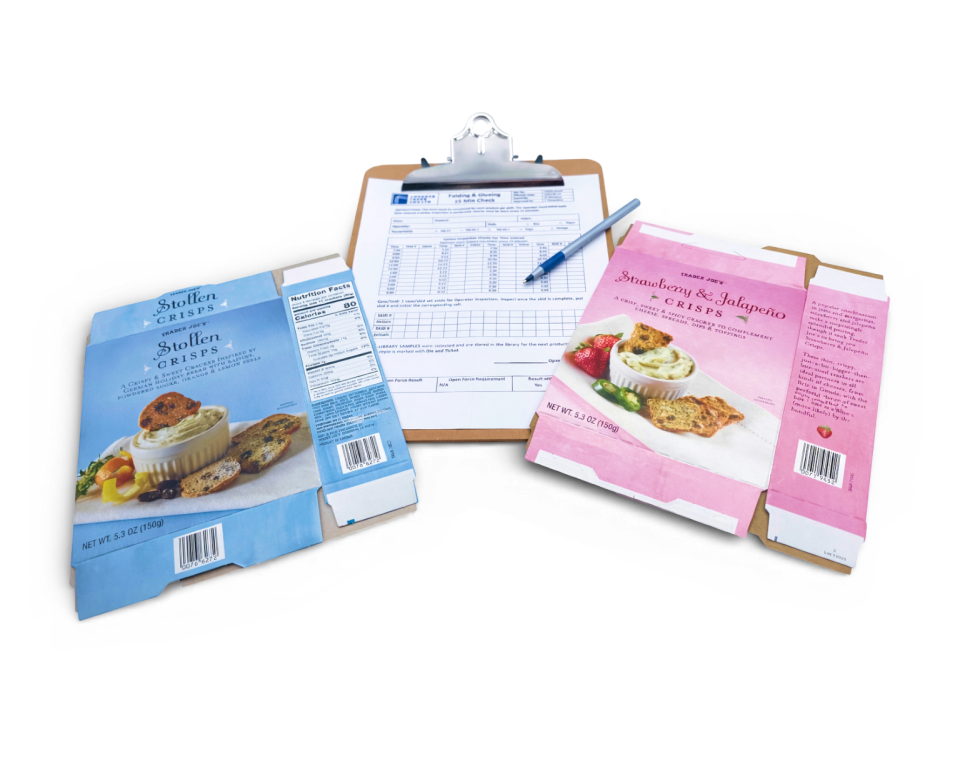
At Advance Paper Box, in-process monitoring ensures quality at every production stage. In sheeting, paperboards are cut to precise dimensions and stacked consistently. Printing is checked for color accuracy, registration, and defects. Die-cutting uses score-bend tests to verify clean cuts and proper folds. Windowing ensures correct placement and adhesion of films, while gluing verifies coverage, bond strength, and box integrity. All inspections, deviations, and corrective actions are documented to maintain consistent quality.

Final inspection & quality control
Final inspection and approval is performed at the end of production to ensure all boxes meet specifications, are structurally sound, and free from defects. Visual inspections verify overall appearance, while dimensional and structural checks confirm proper size, squareness, and alignment of folds, scores, and creases. Functional tests, including bond strength and random stress sampling, ensure durability. Random samples from each batch are compared to approved proofs, and lot numbers are verified for traceability before release.

Continuous quality improvement
At Advance Paper Box, our continuous improvement initiatives enable us to systematically identify defects, inefficiencies, and variations, and implement corrective and preventive actions to enhance overall quality. All nonconformities are carefully documented and analyzed to determine their root causes. Corrective actions address immediate issues, while preventive measures reduce the risk of recurrence. This process is supported by regular internal audits, a preventive maintenance program, and ongoing employee training, ensuring that improvements are consistently applied and sustained.
Material specifications
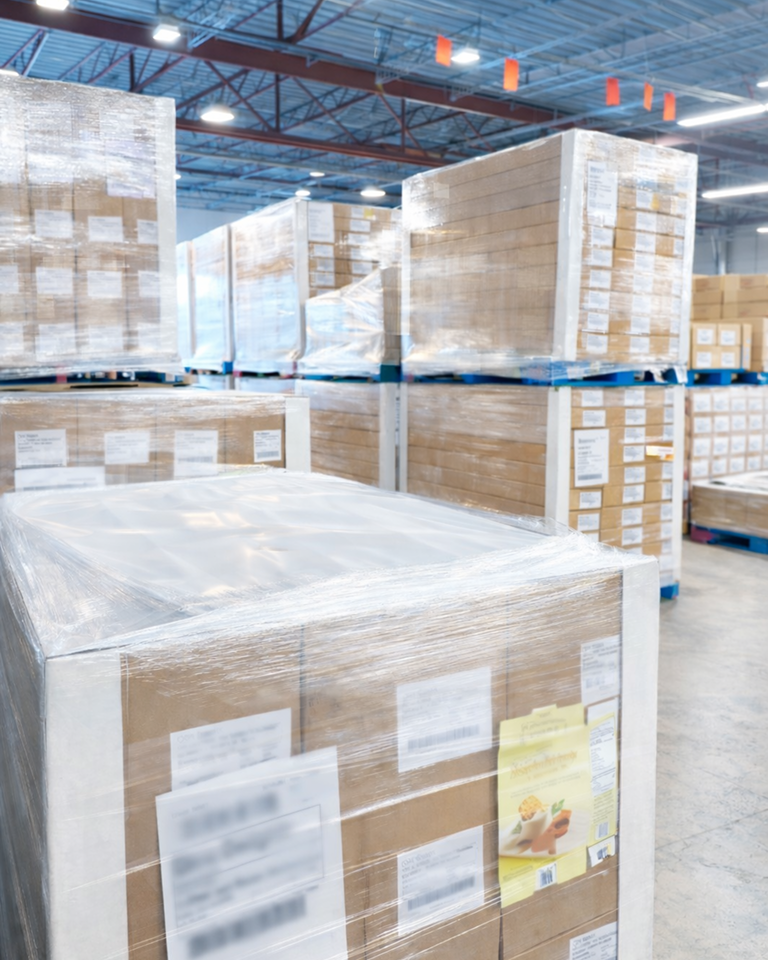
Advance Paper Box enforces strict procedures and guidelines that ensure all raw materials meet quality requirements from the moment they arrive, through storage, to their use in production.
Our material specifications are:

Supplier approval list
A Supplier Approval List is maintained to ensure that all raw materials are sourced from suppliers who consistently meet our quality standards. Approved suppliers are continuously monitored through incoming inspections, defect rates, and delivery performance. Supported by documentation and traceability, this process guarantees a consistent supply of high-quality materials.
Incoming verification
Each shipment of raw materials is inspected for damage, contamination, and conformance to specifications before being released to production, ensuring they meet our strict quality standards. All nonconforming materials are quarantined and reviewed.

Process compatibility
All materials are tested to ensure they perform seamlessly with our equipment and production processes, guaranteeing consistent, high-quality boxes

Controlled storage
All materials are stored in temperature and humidity controlled environments, protected from light and contamination, to maintain their integrity and ensure consistent quality and performance.

Certifications & compliance.
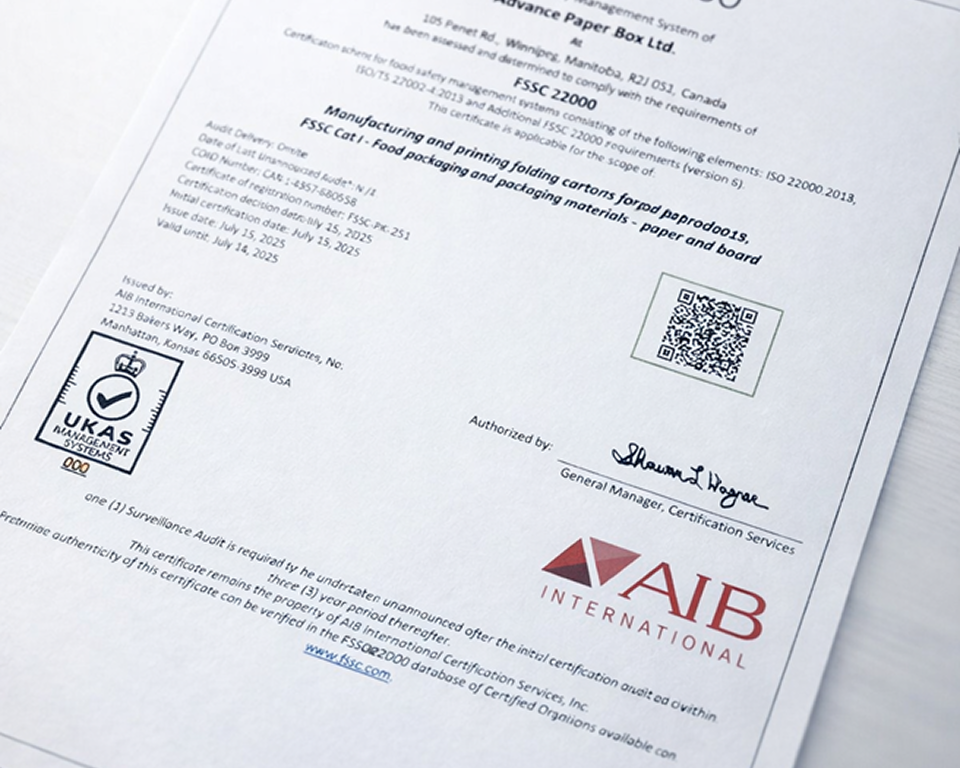
Our customers rely on us to deliver packaging that meets global standards for quality and safety. Advance Paper Box Ltd. operates under a dual-certified management system that ensures control, consistency, and continuous improvement.
Our certification and compliance framework includes:
GFSI-Certified Food Safety System
Advance Paper Box is certified under the Global Food Safety Initiative (GFSI), demonstrating that our packaging meets the highest international standards for quality and food safety. This certification ensures our processes are fully controlled, consistent, and continuously improving to deliver safe, reliable packaging.
Good Manufacturing Practices (GMP)
Advance Paper Box is GMP-certified, ensuring strict quality and safety standards, including personnel hygiene, sanitation, pest control, and equipment maintenance. Our GMP certification gives customers confidence that the products they receive are safe, high-quality, and produced under controlled, reliable manufacturing processes.
Regulatory Compliance
Our regulatory compliance certification demonstrates that our manufacturing processes and products are aligned with legal and industry standards, ensuring our packaging is safe, reliable, and compliant.
Training & Internal Audits
We combine employee training with regular audits to help us meet quality standards and maintain certifications, manage risks, and continuously enhance our processes.

Traceability & batch control.
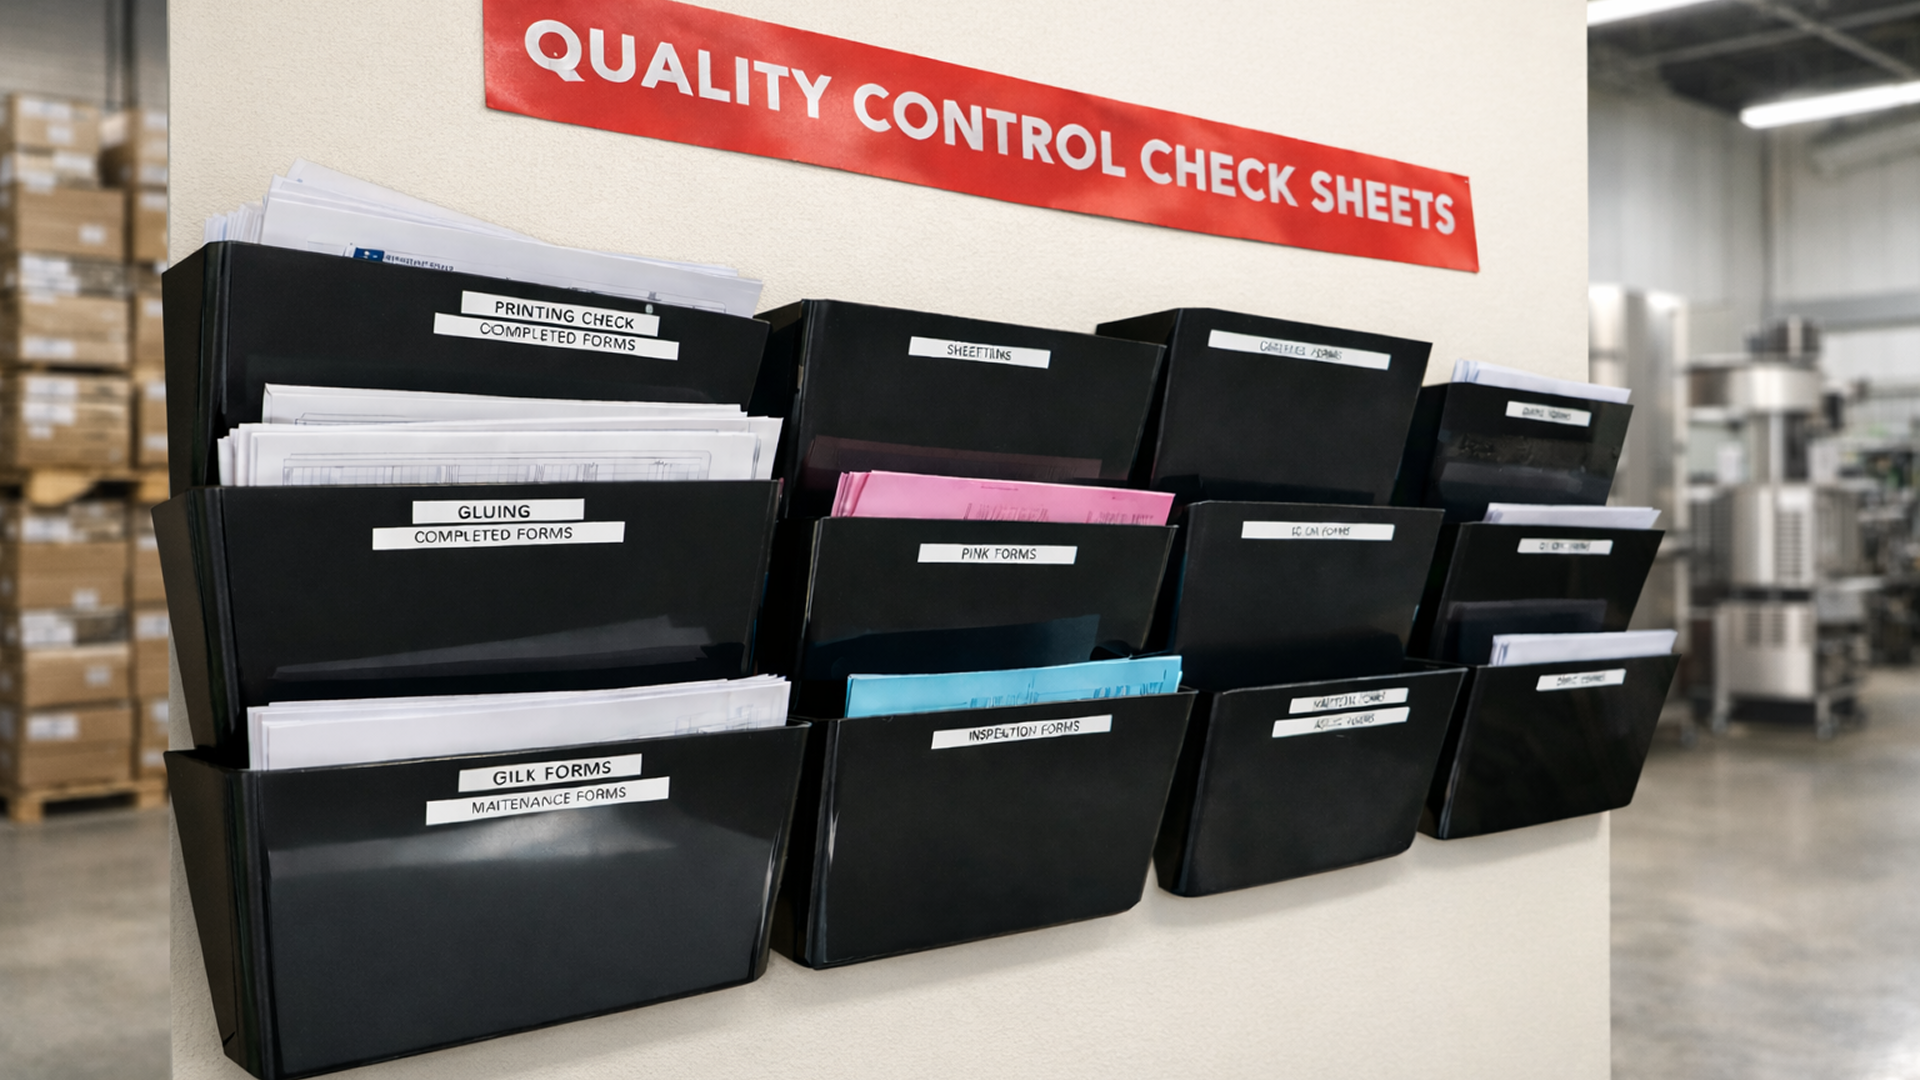
Traceability is a core part of our quality system. Every material, process, and finished product is recorded and linked to its source, ensuring full visibility from receipt through shipment.
Our traceability system provides:
Unique lot identification
Every raw material and finished product batch is assigned a unique lot or batch number, ensuring that each item can be individually tracked throughout the production process.
Complete recordkeeping
Every raw material and finished product batch is assigned a unique lot or batch number, ensuring that each item can be individually tracked throughout the production process.
Hold & release protocols
Our traceability system allows us to quickly identify and isolate any nonconforming materials or products, preventing defects from spreading and ensuring only compliant packaging is shipped to customers. Once isolated, affected items are clearly labeled and investigated before release or proper disposition.
Recall readiness
Through effective lot control and traceability, each product can be traced back to its raw materials, production records, and shipment history. If a quality or safety concern is identified, our recall capabilities enable a rapid, controlled response while maintaining customer confidence and regulatory compliance.
Food safety
In food-contact packaging, food safety is critical to protect consumers and meet regulatory requirements. Our Global Food Safety Initiative (GFSI)–recognized certification ensures that packaging operations follow internationally accepted food safety standards, demonstrating our strong commitment to food safety, product integrity, and compliance.
Our food safety management includes:
HACCP-based controls
We maintain a documented HACCP (Hazard Analysis and Critical Control Points) program, a preventive, risk-based food safety system designed to identify, evaluate, and control potential hazards in food-contact packaging. At Advance Paper Box, HACCP focuses on preventing physical, chemical, and biological contamination.
Facility hygiene standards
Our facility hygiene standards ensure a clean, organized manufacturing environment, free from contamination that could compromise food-contact packaging. Strict hygiene practices help preserve material integrity, product quality, and the safety of our finished packaging
Pest & environmental control
We maintain strict pest management through licensed professionals and implement environmental controls to protect materials and finished packaging. In addition, our preventative maintenance program helps ensure equipment operates reliably, supporting a safe, clean manufacturing environment and consistent product quality.
Improved supplier program
We partner exclusively with approved suppliers who meet rigorous quality standards and have verified compliance with relevant food safety regulations, ensuring all materials consistently support reliable, high-quality packaging.
Training & responsibility
Our comprehensive training program ensures staff understand and uphold their responsibilities while consistently following food safety procedures, GMPs, and HACCP requirements, reducing the risk of contamination and noncompliance.
Quality, safety and innovation in every box
Use the form for general inquiries, project discussions, or to request a callback. Our team will respond as soon as possible.
From streamlining your packaging operations to launching a new product, our team is here to deliver professional support and solutions. Let’s connect.
